Commissioning a compressor or reconnecting one after a motor replacement is routine work, and it is where expensive mistakes happen. Three-phase power has no inherent direction, the air end has no tolerance for a wrong guess, and the time between a reversed start and a ruined rotor pair is measured in seconds.
No, a винтовой компрессор cannot be run backwards. It will turn, but it will not compress: the inlet becomes the outlet, oil stops reaching the rotors, thrust loads reverse, and the air end can be destroyed in under a minute. Industrial packages are built for one direction of rotation only.
The sections below explain what happens inside the machine, how to catch reverse rotation early, and what to do once it has occurred.
What Happens Inside a Screw Compressor When It Runs Backwards
In reverse the machine keeps rotating but stops compressing. The discharge port becomes the suction, the inlet becomes the exhaust, and the oil and thrust systems run against their design direction.
A rotary screw compressor is a positive displacement machine. Two intermeshing rotors trap a fixed volume of air and reduce it as the pocket travels toward the discharge port, which is the definition the Compressed Air and Gas Institute gives for positive displacement compressors. Nothing in that sequence is symmetric: the inlet is shaped for low velocity intake, the discharge port is cut for a fixed volume ratio, and the rotor profile is ground to compress in one direction of travel.
The Compression Cycle Only Works in One Direction
The male rotor drives the female rotor, the lobes unmesh at the inlet to open a cavity, and that cavity is progressively reduced along the rotor length. Pressure rises because volume falls. Reverse the shaft and the pocket forms at the discharge end and grows toward the inlet, so the machine behaves like an expander. No trapped volume is ever reduced against a closed port, so discharge pressure never develops.
Oil Flow and Thrust Load Assume One Direction
Oil injection depends on a pressure difference between the separator tank and the injection point, and some packages add a shaft driven pump for bearings and gears. Running backwards, the compressor cannot build the pressure that drives injection, and a shaft driven pump turns backwards too, so it delivers nothing. The film separating the rotors disappears within the first revolutions, and axial load reverses against thrust bearings preloaded for the opposite direction. The unit then pulls air from the discharge line and pushes it out through the intake filter with the oil mist, so it can sound busy while producing nothing. For a closer look at how the rotor pair builds pressure, see this explanation of rotary screw air ends.
How Do You Know If Your Compressor Is Running Backwards?
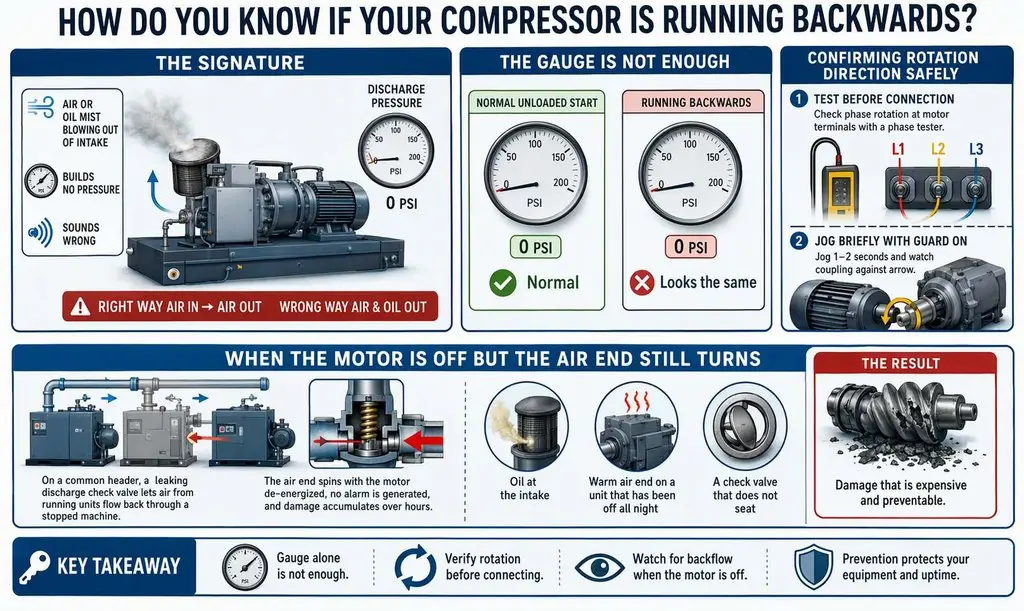
The signature is a compressor that runs, sounds wrong and builds no pressure, with air or oil mist blowing out of the intake instead of compressed air leaving the discharge.
The gauge is the first indicator, but the same reading appears during a normal unloaded start, so confirmation has to come from elsewhere.
| Indicator | Normal start | Reverse rotation |
| Давление на выходе | Rises within seconds | Stays at zero or falls |
| Intake filter housing | Slight inward flow | Air and oil mist blowing out |
| Звук | Rising hum, then smooth load | Grinding, screeching or rattling |
| Вибрация | Low and steady | High and irregular |
| Температура на выходе | Climbs gradually | Spikes almost immediately |
| Ток двигателя | Rises to loaded value | Often stays below loaded value |
| Маслоотделитель | Stable level | Level drops, oil pushed to intake |
| Контроллер | Loads and modulates | Runs without loading |
The motor current row matters most. Because the machine is not compressing, it is not absorbing full load torque, so the overload relay may never trip. An air end can be destroyed while the motor draws less current than in normal service.
Confirming Rotation Direction Safely
Phase rotation testing at the motor terminals before the motor is connected is the only method that prevents the event rather than documenting it. Record the L1, L2 and L3 sequence against the machine, not the panel it came from. Without a meter, jog for one to two seconds with the guard in place and watch the coupling against the arrow on the air end.
When the Motor Is Off but the Air End Still Turns
Not every event is electrical. On a common header, a leaking discharge check valve lets air from running units flow back through a stopped machine. The air end spins with the motor de-energized, no alarm is generated, and damage accumulates over hours. Oil at the intake, a warm air end on a unit that has been off all night, and a valve that does not seat are the usual clues.
What Causes a Rotary Screw Compressor to Run Backwards?
Nearly every case traces back to a reversed three-phase supply at the motor terminals, or to compressed air flowing back through a stationary machine.
The chain of events is short, and it usually starts with a conductor that was moved.
Electrical Work Is the Most Common Trigger
Three-phase motors reverse when any two supply leads are exchanged, and the situations are predictable:
- First commissioning, where the site sequence was never verified.
- Transformer, switchgear or meter base replacement upstream.
- Motor replacement, rewinding, or terminal block reassembly.
- Drive replacement, factory reset or parameter restore.
- Temporary running from a generator during an outage.
- Reconnection after relocation or a panel upgrade.
The compressor is behaving exactly as wired. There is no defect to detect, which is why protection has to be procedural.
Stored Air and a Leaking Check Valve
A check valve that is fouled, worn or mounted too far from the air end lets header pressure reach the rotors whenever the unit stops. On a multi-compressor system, the differential between a loaded header and an idle machine is enough to spin it. A failed or bypassed minimum pressure valve does the same.
Why It Shows Up at Commissioning
Three conditions line up: the wiring just changed, no baseline rotation record exists, and everyone is focused on getting the plant online. Electricians usually verify sequence at the panel they installed, not at the motor, and those points can differ. Assuming a machine that ran correctly before a repair will run correctly after it is the most expensive assumption in a compressor room.
How Much Damage Can Reverse Rotation Cause?
Damage is measured in seconds and concentrates in the air end rather than the motor, which is why the repair bill often resembles a replacement.
| Elapsed time | What happens | Likely outcome |
| 0 to 2 seconds | No pressure, oil mist at the intake | Reversible if stopped at once |
| 2 to 30 seconds | Oil film collapses, rotors contact, thrust reverses | Scoring begins, bearings stressed |
| 30 seconds to 3 minutes | Metal contact, temperature spike, thermal growth | Rotor and casing damage, seal failure |
| 3 to 10 minutes | Clearances close, coating wears through | Seizure, air end scrap |
| After shutdown | Contaminated oil reaches separator and cooler | Secondary damage |
Oil-Injected Versus Oil-Free Outcomes
An oil-lubricated rotary screw compressor relies on injected oil for sealing, cooling and lubrication at once, and reverse rotation removes all three. Rotors are the first casualty, then the shaft seal, then the bearings. Because the oil is also the coolant, temperatures rise fast enough to discolor coatings before any sensor reacts. An oil-free machine fails differently: timing gears protect the rotors briefly, but thrust bearings and gear flanks take the load, and a shaft driven lube pump delivers nothing. The contrast with dynamic machines is instructive, since reverse rotation in centrifugal compressors usually follows a trip and stored gas, while a screw compressor only needs a miswired motor.
Repairable, Rebuildable or Scrap
The decision usually follows the oil. Clean oil after a one second event may mean inspection, new oil, filters and separator. Metal in the oil means the machine comes apart regardless of how it sounds. Scoring on the rotor flanks, a damaged discharge end face, or a rubbed casing is generally terminal, and replacement costs less than a rebuild.
Do Rotary Screw Compressors Run Constantly?
Many do, but continuous running is a control choice rather than a design requirement, and it has no bearing on whether a unit can run backwards.
| Control mode | How it works | Типичные области применения |
| Start and stop | Motor stops when the receiver is full | Small packages, intermittent demand |
| Load and unload | Motor runs, inlet closes at set pressure | Most fixed speed industrial units |
| Modulation | Inlet throttles progressively | Older or specialized units |
| Variable speed | Drive matches speed to demand | Variable demand, efficiency targets |
Continuous operation does create one problem. A unit that runs all shift without loading can look like a compressor facing low demand rather than one running backwards, and background noise hides the sound. The signature is unchanged: no pressure rise, air at the intake, and a temperature trend that does not match the load.

How Long Do Rotary Screw Compressors Last?
A well maintained air end typically reaches 40,000 to 60,000 running hours before overhaul, and the package stays in service for 10 to 15 years, but reverse rotation can consume that life in under a minute.
| Компонент | Typical service interval |
| Oil-injected air end | 40,000 to 60,000 hours |
| Oil-free air end | 25,000 to 40,000 hours |
| Motor bearings | 20,000 to 30,000 hours |
| Separator element | 4,000 to 8,000 hours |
| Смазочный материал | 4,000 to 8,000 hours |
| Муфта | 10 years or more |
Real life depends on duty cycle, ambient temperature, filtration and how consistently the oil is sampled. A unit at full load in a hot, dusty room will not reach the upper end of any range. The point is the scale: tens of thousands of hours of design life against seconds of reverse rotation to erase it.
Common Screw Compressor Problems and How Reverse Rotation Differs
Most screw compressor problems develop over weeks and leave a pressure reading you can work with, while reverse rotation is instant, produces no pressure and announces itself at the intake.
| Problem | Typical symptom | Onset | Pressure behavior |
| High discharge temperature | Alarm, oil discoloration | Gradual | Normal until trip |
| Oil carryover | Oil in filters and downstream lines | Gradual | Normal |
| Separator pressure drop | Rising differential, reduced flow | Weeks | Slightly low |
| Bearing or gear noise | Whine or rumble under load | Weeks to months | Normal |
| Overload trip | Breaker trips under load | Прерывистый | Normal before trip |
| Intake valve fault | Will not load or unload | Sudden | Low or unstable |
| Reverse rotation | Air and oil mist at intake | Immediate | Zero, or falling |
Overheating is the most confused case, because both events raise temperature quickly. The difference is that rotary screw compressor overheating still produces pressure and trips on a setpoint, while reverse rotation never reaches normal pressure.
Telling Reverse Rotation Apart From a Normal Fault
Three questions settle it. Did the machine build any pressure at all? Is air or oil mist coming out of the intake? Has anything electrical changed in the last 24 hours? A yes to the second and a no to the first is enough to stop the machine and check phase sequence, whatever the controller reports.
How to Prevent Reverse Rotation
Prevention is a commissioning discipline rather than a device. Verify the sequence at the motor, record it, label the conductors, and never assume a reconnect preserved the original wiring.
Three layers matter: what the electrician verifies, what the piping protects, and what the startup routine confirms.
Electrical Commissioning Rules
Measure phase sequence at the motor terminals, not at the panel, and file the reading with the date and instrument used. Tag L1, L2 and L3 on both ends of every conductor before disconnecting, and photograph the terminal block. Fit a phase sequence relay where the process justifies it, so a reversed feed prevents a start instead of causing one.
Mechanical Safeguards on the Discharge Side
Mount the check valve as close to the air end or separator outlet as layout allows, outside any maintenance bypass. Test it at every major service, confirm the minimum pressure valve holds, and make sure no procedure requires an air end to be spun by header pressure.
A Startup Checklist That Actually Gets Used
- Confirm phase sequence at the motor terminals and record it.
- Confirm the arrow on the air end matches expected shaft direction.
- Jog for one to two seconds and watch the coupling, not the gauge.
- Start unloaded with the discharge isolation valve closed.
- Monitor pressure, temperature, current and sound through the first load cycle.
- Log baseline readings for the next intervention to compare against.
What to Do After a Reverse Rotation Event
Stop the machine, isolate it and do not restart until the oil and the air end have been inspected, because a second start turns a repairable air end into scrap.
The response has three phases: stop the damage, measure it, then decide whether the air end can stay.
Immediate Actions
- Stop from the controller, then open the upstream breaker.
- Apply lockout and tagout, and close the discharge isolation valve.
- Do not attempt another start to confirm the diagnosis.
- Record duration, indications, and whether the motor was newly wired.
- Draw an oil sample before draining and keep it for analysis.
- Notify the supplier before dismantling anything that affects warranty.
Inspection Checklist
| Пункт | What to look for | Action if abnormal |
| Смазочный материал | Metal particles, discoloration | Full teardown before restart |
| Oil filter and separator | Metal debris, collapsed media | Replace, find the source |
| Intake housing | Oil mist residue | Clean, confirm cause |
| Rotor surfaces | Scoring, coating wear | Borescope, then repair |
| Rotor end clearance | Out of specification | Air end service |
| Coupling and alignment | Wear, offset | Replace and realign |
| Двигатель | Insulation resistance | Test before reconnection |
| Check and minimum pressure valves | Seat damage | Replace |
A borescope through the intake and discharge ports usually decides whether the air end must come out. Any metal in the oil settles the question.
Restart Criteria
Restart only when oil analysis is clean, the air end has been inspected and cleared, the lube circuit has been flushed, filters and separator replaced, the motor has passed insulation and resistance tests, alignment is verified, and phase sequence has been re-checked. Run the first cycle unloaded and sample the oil again at 50 hours. A structured air compressor maintenance guide is a reasonable baseline for what follows.
Часто задаваемые вопросы
Three questions come up repeatedly once operators understand the mechanism, and the answers below extend the discussion rather than repeat it.
Can a VFD prevent a rotary screw compressor from running backwards?
No. A drive controls speed and torque, not the physical direction of the motor connected to it. Swap two motor leads and most drives will produce a reversed rotating field without complaint. Some detect phase loss or abnormal current, but none of that replaces a phase sequence check at commissioning.
Does running a compressor backwards void the warranty?
Usually the damage is classified as an installation or commissioning error rather than a material defect, which removes it from coverage. Suppliers typically ask for the commissioning record, the phase sequence reading and the oil sample before deciding. A signed commissioning sheet with recorded phase sequence is the cheapest warranty protection available.
Is reverse rotation the same as unloading?
No. Unloading is normal operation: the inlet valve closes, the compressor keeps turning in the correct direction at low output, and oil circulation and cooling continue. Reverse rotation has the opposite airflow, no oil delivery, no pressure and immediate mechanical damage. An unloaded compressor is quiet and stable. A reversed one is loud, hot and producing air at the wrong end.